


High-Salinity Wastewater Treatment Technologies Compared
Release Time:
2026-09-07 11:46

High-Salinity Wastewater Treatment Technologies Compared
High-salinity wastewater is one of the hardest streams to treat: salt levels above 20,000 mg/L suppress biological activity, so conventional biological processes fail quickly. Treatment demands a combination of softening, membrane concentration, and evaporation crystallization. This article compares the main technologies, explains how to choose the right train for your water, and covers the special case of RO brine.
What Counts as High-Salinity Wastewater
High-salinity wastewater is generally defined as water with total dissolved solids (TDS) above 2%, or 20,000 mg/L. It is common in coal chemical plants, chemical industry, textile dyeing, landfill leachate treatment, and power plant desulfurization. Because high salt inhibits microorganisms, a combination route of pretreatment softening, membrane concentration, and evaporation crystallization is required to achieve volume reduction, resource recovery, and zero liquid discharge.

Step 1: Pretreatment — Softening and Silica Removal
Lime and soda ash with flocculants remove calcium, magnesium, silica, suspended solids, and part of the organics, protecting downstream membranes and evaporators from scaling. Ultrafiltration is added where finer suspended solids removal is needed.
Step 2: Membrane Concentration Technologies Compared
Nanofiltration (NF) selectively separates divalent ions, while reverse osmosis (RO) and electrodialysis (ED) concentrate wastewater from TDS 2% to 3% up to 8% to 15%, with recovery rates of 60% to 90%. Membrane concentration shrinks the downstream evaporation load dramatically and reuses the permeate. NF also enables split-salt recovery: a mixed salt stream can be separated into high-purity sodium chloride and sodium sulfate products.
For RO brine with TDS of 40,000 to 50,000 mg/L, high-pressure reverse osmosis (HPRO) using high-pressure-resistant membrane elements at 6 to 12 MPa can further concentrate the stream to TDS of 80,000 to 120,000 mg/L, cutting the downstream evaporation volume by more than 50%. Electrodialysis and bipolar membrane electrodialysis suit medium-concentration brine and can even produce acid and alkali, but capital cost is relatively high.
Step 3: Evaporation Crystallization
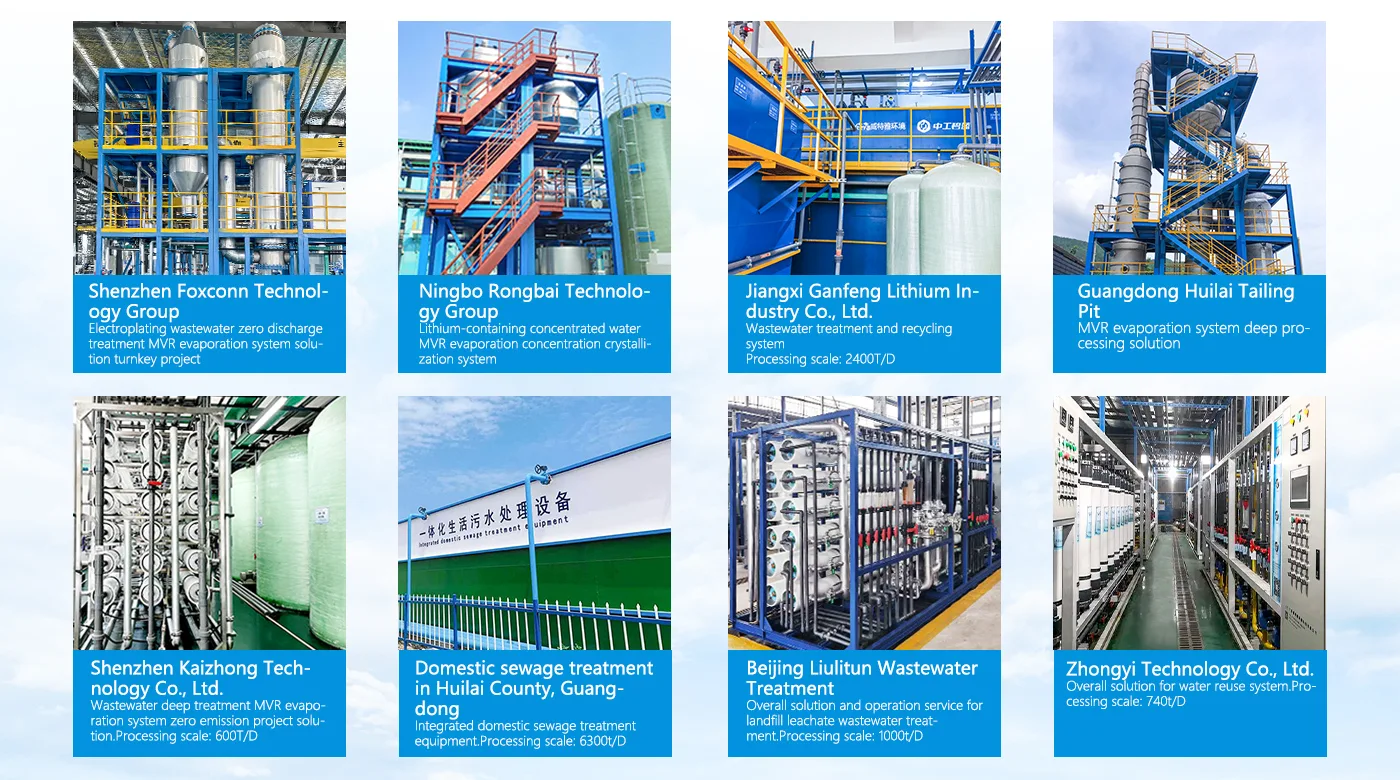
The concentrate enters an MVR evaporator or multi-effect evaporator for further concentration to supersaturation, after which a crystallizer produces salt crystals. MVR evaporator systems consume roughly 40 to 70 kWh per ton of water evaporated and save more than 70% of energy compared with single-effect evaporation. With split-salt crystallization, the product salt purity reaches 97% or higher, turning a disposal cost into saleable by-product revenue.
Mother Liquor and Overall Recovery
Mother liquor from the crystallizer returns for re-concentration or enters a mixed-salt drying unit. Whole-plant water recovery reaches 95% to 98% with mixed salt kept at 5% to 15%, which is what makes true zero liquid discharge (ZLD) systems achievable.
How to Choose the Right Treatment Train
Selection depends first on TDS and ionic composition. For brine below TDS 50,000 mg/L, HPRO re-concentration followed by evaporation is often the most economical. Above TDS 50,000 mg/L, direct MVR evaporation crystallization is usually cheaper. Organic content matters too: when COD is high, add advanced oxidation (ozone catalytic oxidation, Fenton, or electrochemical oxidation) before evaporation to prevent foaming and discoloration of the salt. Finally, match the goal to local discharge standards and solid-waste policy: compliant discharge, partial reuse, or full zero liquid discharge.
Because high-salinity water quality varies enormously by industry, a full water analysis and pilot test should always precede the final process design. WTEYA brings 20 years of experience and more than 100 delivered zero-discharge projects in high-salinity treatment, and offers complete wastewater treatment solutions from water quality testing, pilot validation, and process design to equipment manufacturing and operation and maintenance.
Frequently Asked Questions
Q: How does industrial wastewater treatment work?
A: Industrial wastewater treatment typically involves pre-treatment, membrane concentration, evaporation, and crystallization to remove contaminants and recover water.
Q: What are the benefits of wastewater recycling?
A: Benefits include reduced water costs, environmental compliance, reduced discharge fees, and improved corporate sustainability.
Ready to Start Your Project?
Join industry leaders like Foxconn, BYD, and Huawei who trust WTEYA for their critical wastewater treatment needs.
Get the same expertise working for your wastewater treatment facility. Contact us now.
📱 WhatsApp: +86-1800 2840 855
✉ Email: info@vteya.com
🌐 Website: www.vteya.com
Front page of Cross
Next go-to page
Related information
MVR Evaporator Condensate Reuse: Quality and Options
MVR Evaporator Condensate Reuse: Quality and Options The condensate produced by an MVR evaporator is not a waste stream to be disposed of — it is distilled water of consistent quality.
MVR Evaporator Troubleshooting: Common Problems and Fixes
MVR Evaporator Troubleshooting: Common Problems and Fixes MVR evaporators are mechanically simple compared with steam-driven evaporator trains, but they are sensitive to small changes in vacuum, scaling and compressor stability.
Crystallization for Battery Material Wastewater Recovery
Crystallization for Battery Material Wastewater Recovery Battery manufacturing is a wet chemistry business. Cathode active material plants producing lithium iron phosphate or nickel-cobalt-manganese chemistries, and hydrometallurgical recycling lines recovering metals from spent cells, all consume...
WTEYA 4021 Desalination Systems Reach Four Global Markets
WTEYA 4021 seawater desalination systems reach four global markets in one batch, with shipments to the United States, Greece, Colombia and Peru covering the Americas and Europe.
How Automated Is an MVR Evaporator? PLC Control
How Automated Is an MVR Evaporator? PLC Control An MVR evaporator is the most automated category of evaporation equipment in service today.
Tubular Heat Exchanger vs Plate: Which for Your Evaporator?
Tubular Heat Exchanger vs Plate: Which for Your Evaporator? In almost every MVR evaporator and forced circulation evaporator, the heat exchanger is where the plant economics are decided.
Guangdong WTEYA Environmental Technology Co., Ltd
Contact us
WhatsApp: +86 1800 2840 855
Tel: +86-0769-28636053
+86-0769-28636126
Email: info@wteya.com
Add: Floor 14, F4 building, TianAn digital town,
Nancheng District, Dongguan,Guangdong, China